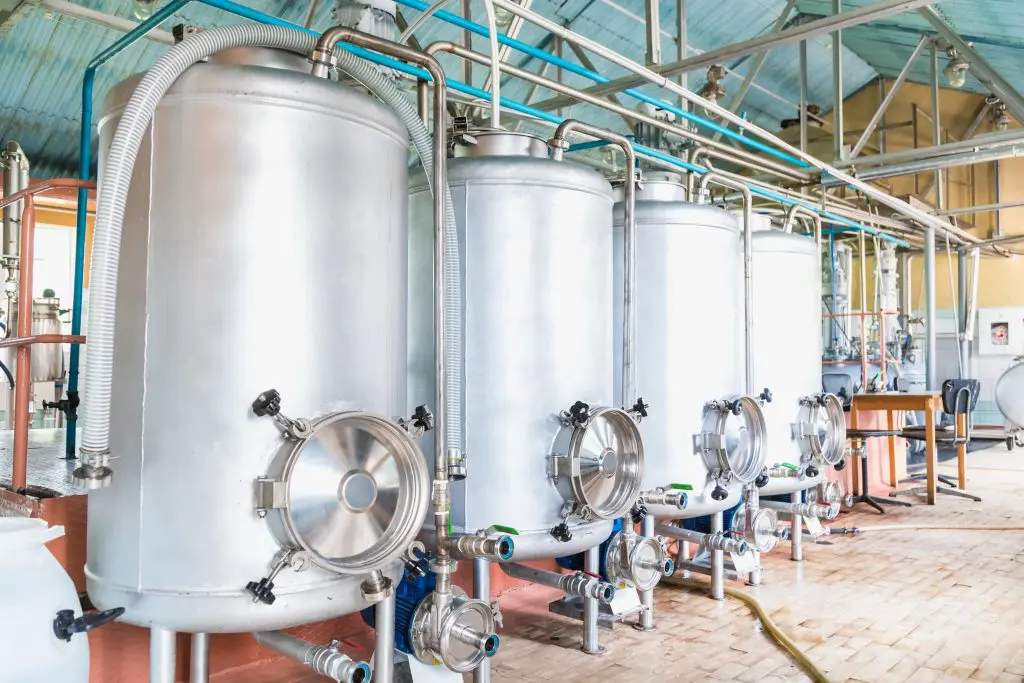
Manufacturing, pharmaceutical, biomedical, biotechnology, and chemical facilities face a wide range of fire hazards across production areas, laboratories, chemical storage facilities, warehouses, and electrical infrastructure. Flammable liquids, combustible dust, reactive chemicals, industrial machinery, and specialized equipment can create complex fire risks that require carefully engineered protection solutions.
Manufacturing & Industrial Fire Risks
Industrial environments require a thorough understanding of the materials, equipment, and processes involved in daily operations. Identifying potential ignition sources and assessing the hazards associated with production, chemical handling, and storage are essential to developing an effective fire protection strategy.
Chemical Storage and Handling Hazards: Manufacturing and chemical facilities may store and handle flammable solvents, reactive reagents, volatile compounds, and other hazardous substances. Improper storage, accidental releases, or contact between incompatible chemicals can trigger fires, dangerous reactions, or explosions. Appropriate fire protection measures must account for the properties of the substances involved and the conditions in which they are stored and used.
Laboratory and Clean Production Environments: Pharmaceutical, biomedical, and biotechnology facilities often include laboratories, research areas, and controlled production environments. These spaces may contain flammable chemicals, specialized equipment, and sensitive materials that require specific fire protection considerations. Systems must be selected according to the hazards present while accounting for personnel safety, equipment protection, and applicable standards, including NFPA 45 for laboratories using chemicals where relevant.

Combustible Dust and Fire Hazards: Fine particles generated during manufacturing processes can accumulate on surfaces or become suspended in the air. Under certain conditions, combustible dust can ignite or cause an explosion. Facilities handling combustible powders and other particulate materials require appropriate hazard assessments and protection measures tailored to their processes and equipment.
Electrical Systems and Industrial Machinery: Manufacturing operations depend on electrical distribution systems, motors, control panels, automation equipment, and heavy machinery. Electrical faults, overheating, mechanical failures, and friction can introduce ignition sources that threaten personnel, equipment, and production continuity. Fire protection systems must address the specific risks associated with these installations.
Flammable Materials and High-Hazard Operations: Facilities handling flammable liquids, gases, combustible solids, or other high-hazard materials may face fire scenarios that require more than a conventional automatic sprinkler system. Depending on the hazard, specialized suppression solutions may be needed to control rapidly developing fires, protect high-value assets, and reduce the potential for fire spread and re-ignition.
Fire Detection and Suppression Solutions for Manufacturing & Industrial Facilities
Viking Fire Protection provides fire protection systems designed around the specific hazards and operational requirements of industrial environments. Solutions are selected according to the facility’s processes, materials, equipment, building characteristics, and applicable codes and standards.
Fire Extinguishers: Portable fire extinguishers provide an important first line of response for incipient fires. Viking helps ensure that extinguishers are selected, positioned, inspected, and maintained according to applicable requirements, including NFPA 10. In laboratory environments, NFPA 45 may also apply to fire protection considerations involving laboratories that use chemicals.
Sprinkler Systems: Automatic sprinkler systems are designed to control or suppress fires based on the hazards present within a facility. Manufacturing and industrial applications require careful consideration of occupancy, storage arrangements, combustible materials, and process conditions. Viking designs and installs sprinkler systems tailored to these requirements and applicable standards.
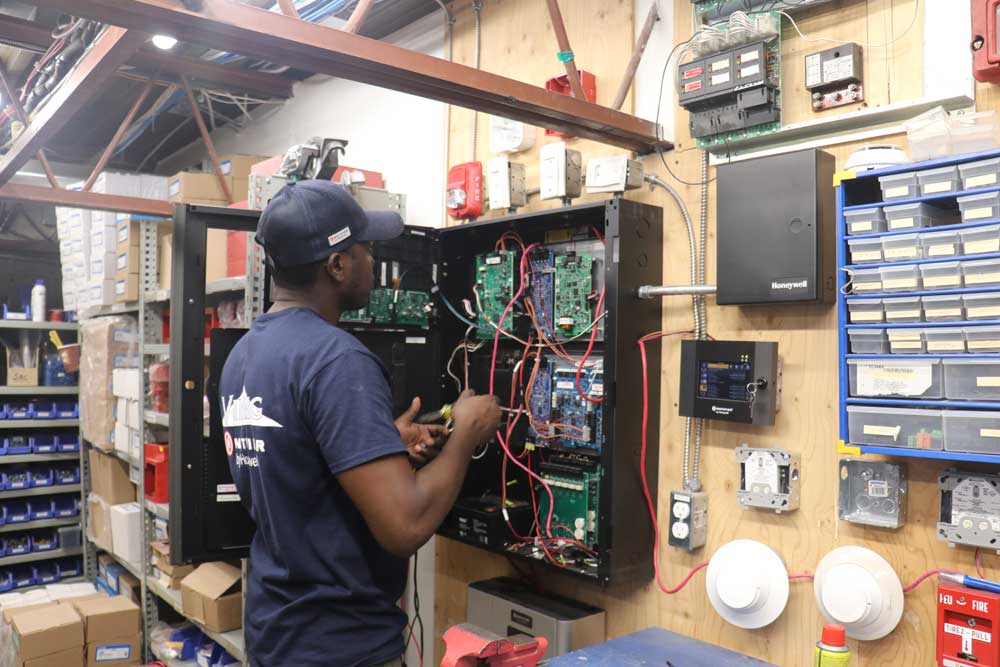
Fire Alarm Systems: Early detection and notification are essential in manufacturing plants, chemical facilities, laboratories, and production environments. Viking provides fire alarm installation, inspection, testing, and maintenance services to help ensure systems are suited to the facility’s layout, occupancy, and operational requirements. Applicable standards, including CAN/ULC-S524, CAN/ULC-S537, and CAN/ULC-S536, are considered according to the work being performed and the jurisdiction.
Special Hazard and Clean Agent Suppression Systems: Certain industrial applications require specialized suppression solutions to address hazards that conventional sprinkler systems may not adequately manage on their own. Clean agent systems may be suitable for protecting sensitive electronic equipment, control rooms, and other critical assets where appropriate. Other specialized systems can be considered for areas involving flammable liquids, combustible materials, or specific industrial processes.
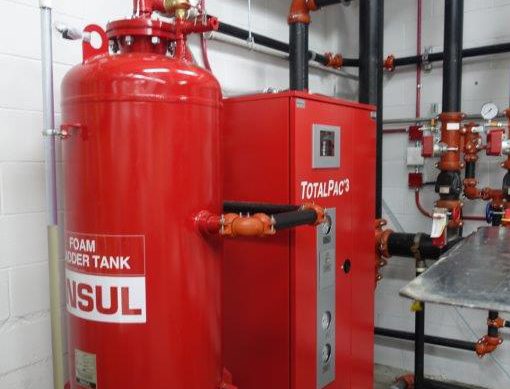
Foam Fire Suppression Systems: Foam suppression systems like the FireFlex® ICAF can be used in industrial applications involving flammable liquids and other hazards for which foam is an appropriate extinguishing agent. Depending on the application and design requirements, low-expansion, medium-expansion, or high-expansion foam systems may be considered.
By forming a blanket over burning liquids or combustible surfaces, appropriately selected foam systems can help suppress flames, limit the release of flammable vapours, and reduce the risk of re-ignition. System design must account for the hazard, the materials involved, environmental considerations, and applicable requirements.
TRUST VIKING’S EXCELLENCE
Complete Range of Fire Protection Services
Whether you need design, installation, inspection or maintenance of fire protection systems, Viking is the name that you can trust.
SOLUTIONS FOR ALL TYPES OF RISKS
Our solutions
We offer services that cover all aspects of the fire protection and design-build process, engaging the client at every step to ensure the best experience possible.
OUR SUCCESSFUL PROJECTS
We have the solution for your project
Smurfit WestRock – Montréal
Smurfit WestRock is a major player in sustainable packaging and paper manufacturing, requiring robust safety infrastructure to support its large-scale operations. The project focused on ensuring trustworthy fire protection across the site to meet stringent safety and operational standards.
Viking was responsible for the installation of a complete fire loop system. Our team provided end-to-end execution, coordinating design integration and on-site installation to deliver a dependable system that enhances fire safety and long-term facility protection.
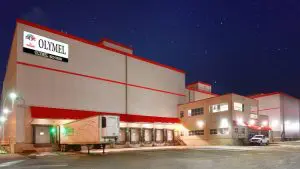
Olymel – Red Deer, Alberta
The Olymel plant in Red Deer, Alberta, plays a critical role in Canada’s food processing industry, operating within demanding environmental and safety regulations. The project aimed to strengthen fire protection for the facility’s perimeter and freezer areas to ensure continuous, safe production operations.
Viking handled the design, supply, and installation of two levels of sprinkler lines throughout the plant’s perimeter. In addition, our team designed and supplied a dedicated water tank and pump house to provide complete perimeter protection, especially for freezer zones. The integrated fire protection system reflects Viking’s commitment to safety, performance, and customized engineering solutions.
READY TO PROTECT YOUR
MANUFACTURING PROJECT?
Contact Viking Fire Protection to request a quote or to learn about how we can help your organization.
"*" indicates required fields